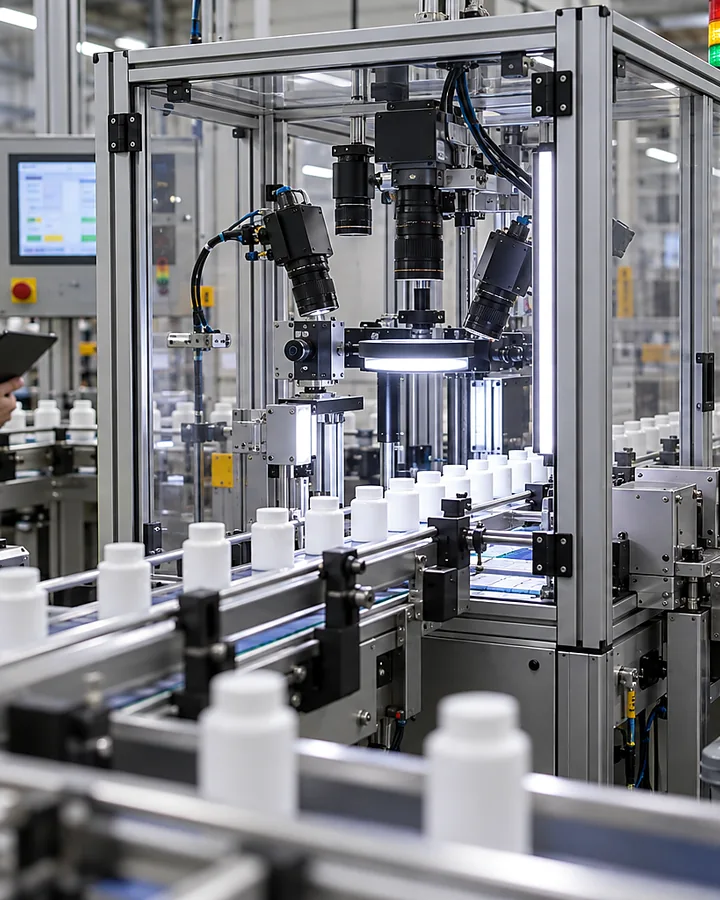
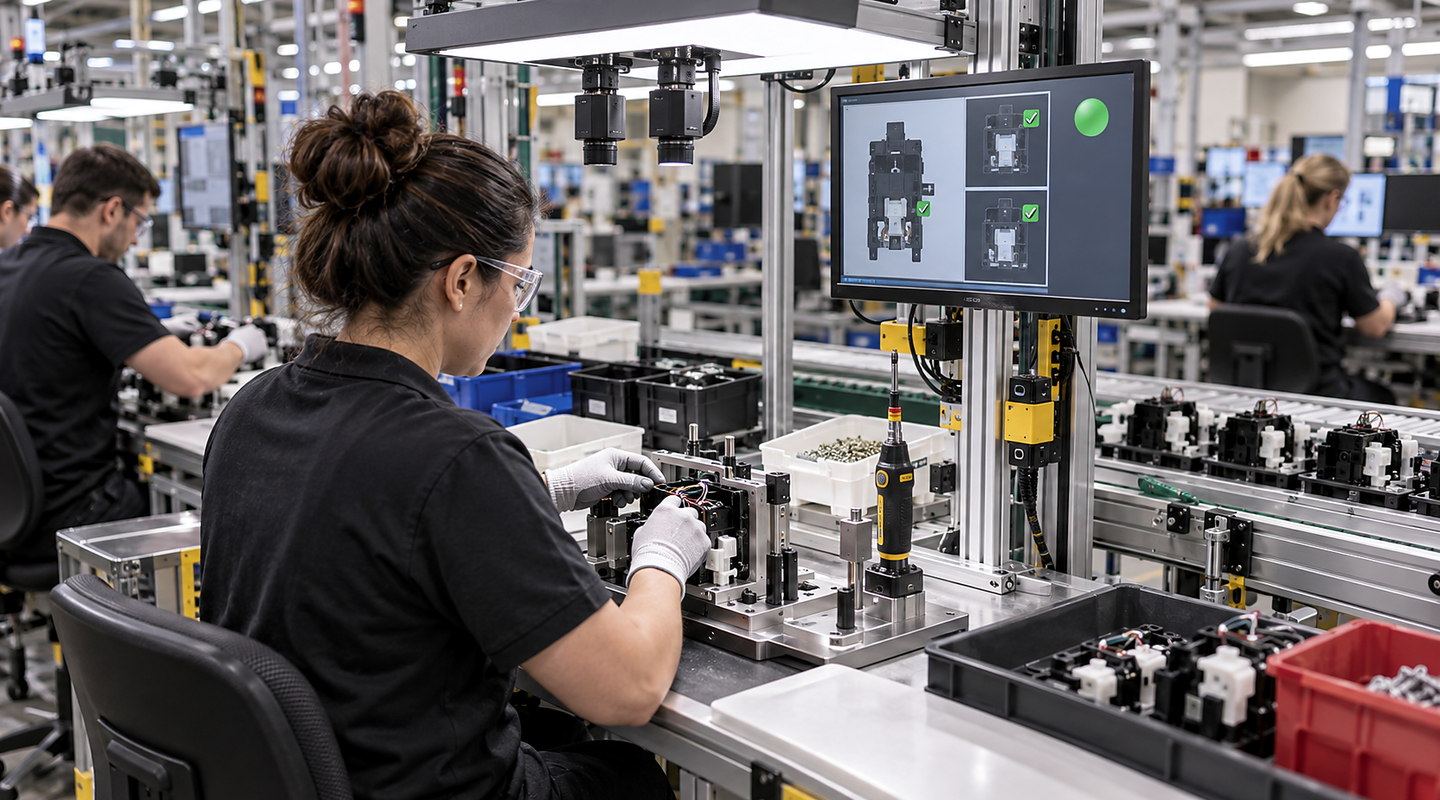
Person handling a component at a workstation beneath cameras beside a screen displaying component images.
Industrial machine vision

Gasket Presence Inspection

Plan gasket presence inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems.

Speak directly with Oxford Vision Systems about gasket presence and position checks.

Quick answer

How can we verify that a gasket is present and correctly positioned?

Separate presence from position, seating and damage in the inspection specification. Supply assemblies showing correct gaskets, missing sections, twists and displaced examples where relevant. Check which features are visible after assembly and agree the camera views, location method and response when a decision cannot be made confidently.

Person handling a component at a workstation beneath cameras beside a screen displaying component images.
Person holding a tablet beside an inspection camera and small metal components on a conveyor.
Six useful questions

Describe what you need from gasket presence inspection before choosing a solution

For in-line inspection using gasket presence and position checks, share the normal condition, realistic range and difficult cases the finished system must handle.

Question 1

Visible Defect or Measurement Definition for Gasket Presence & Position Checks

For your initial enquiry about gasket presence inspection, describe the current position, required outcome, acceptable limits and known exceptions for visible defect or measurement definition for gasket presence & position checks. That lets us compare options against your real production rather than one nominal value.

Question 2

Good, Bad and Marginal Sample Range

For your initial enquiry about gasket presence inspection, describe the current position, required outcome, acceptable limits and known exceptions for good, bad and marginal sample range. That lets us compare options against your real production rather than one nominal value.

Question 3

Part Presentation and Production Speed

For your initial enquiry about gasket presence inspection, describe the current position, required outcome, acceptable limits and known exceptions for part presentation and production speed. That lets us compare options against your real production rather than one nominal value.

Question 4

Optics, Lighting and Environmental Conditions

For your initial enquiry about gasket presence inspection, describe the current position, required outcome, acceptable limits and known exceptions for optics, lighting and environmental conditions. That lets us compare options against your real production rather than one nominal value.

Question 5

Recipe, Reject and Line-Control Interfaces

For your initial enquiry about gasket presence inspection, describe the current position, required outcome, acceptable limits and known exceptions for recipe, reject and line-control interfaces. That lets us compare options against your real production rather than one nominal value.

Question 6

False-Accept, False-Reject and Challenge Criteria

For your initial enquiry about gasket presence inspection, describe the current position, required outcome, acceptable limits and known exceptions for false-accept, false-reject and challenge criteria. That lets us compare options against your real production rather than one nominal value.
Applications

Two useful starting points for gasket presence inspection

The right choice changes with visible defect or measurement definition for gasket presence & position checks, good, bad and marginal sample range, your line layout and required results.

What happens next

Your route from an initial enquiry to a working solution

You can review decisions about recipe, reject and line-control interfaces and false-accept, false-reject and challenge criteria at each stage.

  1. 01

    Define the Visible Decision and Collect Representative Samples

    Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for gasket presence & position checks and the difficult good, bad and marginal sample range cases.

  2. 02

    Prove Contrast, Presentation and Timing in an Optical Trial

    Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.

  3. 03

    Integrate Cameras, Controls, Reject Handling and Recipes

    Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.

  4. 04

    Challenge Marginal Cases and Document Agreed Results

    Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.

Important limits

Know what needs a separate check

Your final solution for gasket presence and position checks must reflect the law, current standards and site-specific risks that apply to your installation.