Requirement
Define separate presence, position, visible seating and damage boundaries and the intended handling of failed or uncertain results. Identify hidden and functional properties that need another test.
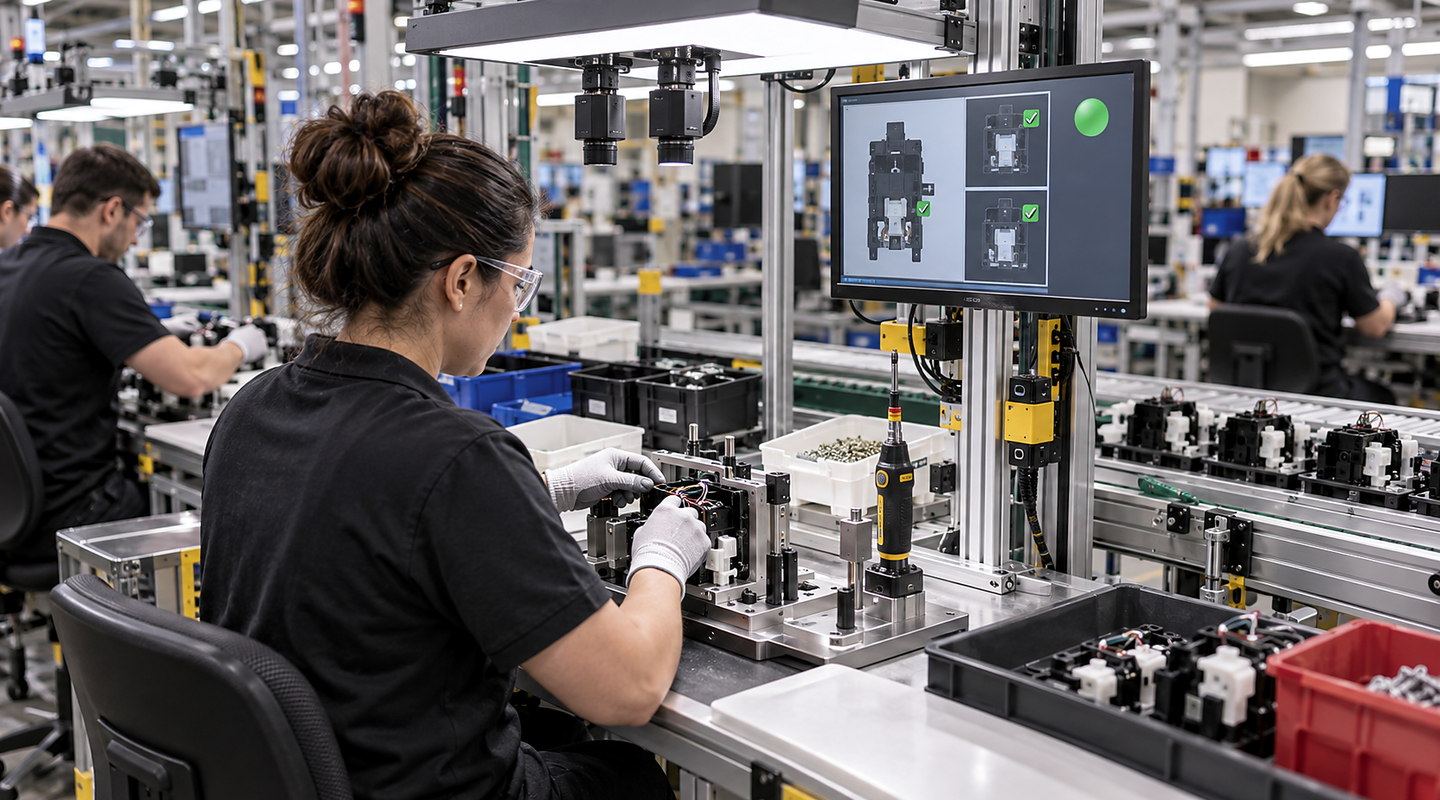
Specify gasket inspection with separate visible checks, identified sample decisions, camera views, location method, line interfaces and failed or uncertain-result handling.
Specify separate gasket presence, position, visible seating and damage decisions, with identified correct and relevant missing-section, twisted, displaced and marginal assemblies. State which features are visible after assembly, the proposed camera views and location method. Agree representative running conditions, interfaces, challenge records and the response to an uncertain decision.
Use the same option-comparison criteria and sample-based acceptance plan. Keep confirmed requirements, hidden or functional exclusions and conditions still needing an optical trial separate.
Plan gasket presence inspection around representative good, bad and marginal samples, line presentation, lighting, reject handling and challenge criteria. Discuss an optical feasibility trial with Oxford Vision Systems. A clear brief should state the operating range for visible defect or measurement definition for gasket presence & position checks and your requirements for false-accept, false-reject and challenge criteria.
Discuss your application
Define separate presence, position, visible seating and damage boundaries and the intended handling of failed or uncertain results. Identify hidden and functional properties that need another test.
Provide identified correct and relevant missing-section, twisted, displaced and marginal assemblies. State actual presentation, camera-visible features, location variation and representative timing and speed.
Compare expected and recorded decisions using the agreed views, location method, setup and repetitions. Retain false accepts, false rejects, uncertain cases, assembly/result association and the observed handling response.
For gasket presence inspection, use “shall” only for a requirement that can be demonstrated. Keep preferences, assumptions, provisional line connections and future options clearly separate.
Your final gasket presence inspection scope must also account for recipe, reject and line-control interfaces, false-accept, false-reject and challenge criteria, current regulations and the conditions at your site.